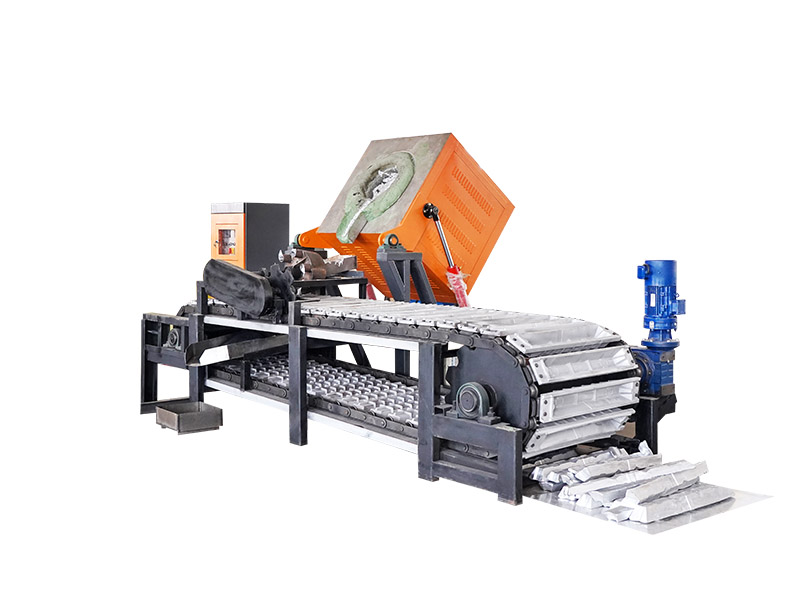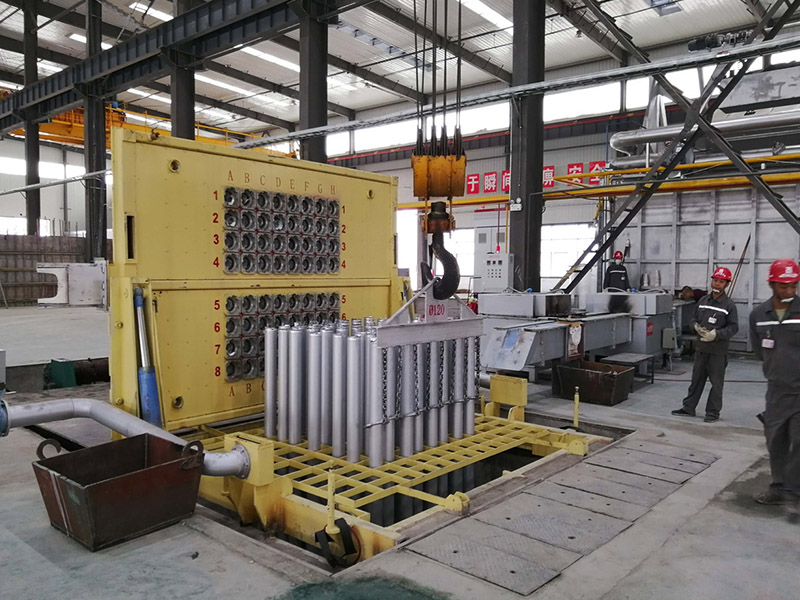
Foundry sand reclamation equipment is a process investment, not simply a standalone machine purchase. The right system helps a molding operation recover usable sand, manage fines and contaminants, and make the return loop more predictable. The wrong scope can create bottlenecks, unstable sand properties, or costly maintenance access problems. Procurement and engineering teams should start with the binder system, sand flow, production pattern, and quality targets, then specify a reclamation line that fits the whole molding process.
Start with the sand system, not the reclaimer alone
Reclamation begins after shakeout but influences every later stage of sand preparation. Feed material can vary in temperature, lump size, binder residue, coatings, metal contamination, and moisture. A useful specification records these conditions across normal and peak production, rather than relying on a nominal tonnage figure.
Map the material path from shakeout through screening, transport, cooling, reclamation, storage, and return mixing. This makes it easier to identify where capacity, dust control, sampling, or access may limit the project.
At this stage, walk the proposed route with production, maintenance, quality, and safety representatives. Each group sees a different constraint: production sees changeover pressure, maintenance sees wear access, quality sees variation in the return stream, and safety sees traffic and isolation points. A short shared review often prevents expensive late changes to conveyors, platforms, or collection connections.
Choose mechanical or thermal reclamation by the requirement
Mechanical reclamation uses attrition and separation to remove loose binder residue and break down lumps. It can be a practical fit when the target reuse level and binder system allow it. Thermal reclamation adds a controlled heating stage to address more persistent organic residues, with corresponding requirements for energy, emissions management, and safe operation.
The choice should follow test results and the intended reuse ratio. Neither method should be selected solely because it is familiar to an existing plant.
Define throughput as a range with surge capacity
Design throughput around the actual shift pattern, casting mix, and shakeout peaks. A system sized only for average flow may force operators to bypass steps or create piles that change feed consistency. Include expected startup, changeover, and maintenance conditions in the capacity discussion.
- Average and peak sand return per hour
- Maximum casting or flask load at shakeout
- Required reclaimed-sand storage time
- Available floor space, elevation, and maintenance clearance
These details also help integrate reclamation with a sand mold casting production line without adding unnecessary transfers or handling points.
Control quality with defined measurements
Recovered sand should be evaluated against the requirements of the molding process, not just against a visual inspection. Agree in advance on sampling location, frequency, and the indicators used to decide whether reclaimed sand is ready to return. The relevant limits are specific to the sand, binder, and casting quality requirements.
Define who reviews the data and what happens when a result falls outside the agreed window. A practical response may include changing the reclaimed-sand proportion, inspecting a separator or classifier, or holding material for further evaluation. The important point is to connect the measurement to a controlled decision rather than treating laboratory work as an isolated activity.
Keep trial records separate for new sand, mixed sand, and reclaimed material. Trend data is more useful than a single favorable test because it reveals changes in feed or equipment condition.
Traceability is especially valuable when a casting-quality issue appears after a shift change or a new return stream enters the system. A concise log of feed source, operating conditions, test results, and corrective actions lets the team investigate the actual sequence instead of relying on recollection.
Build dust and maintenance access into the layout
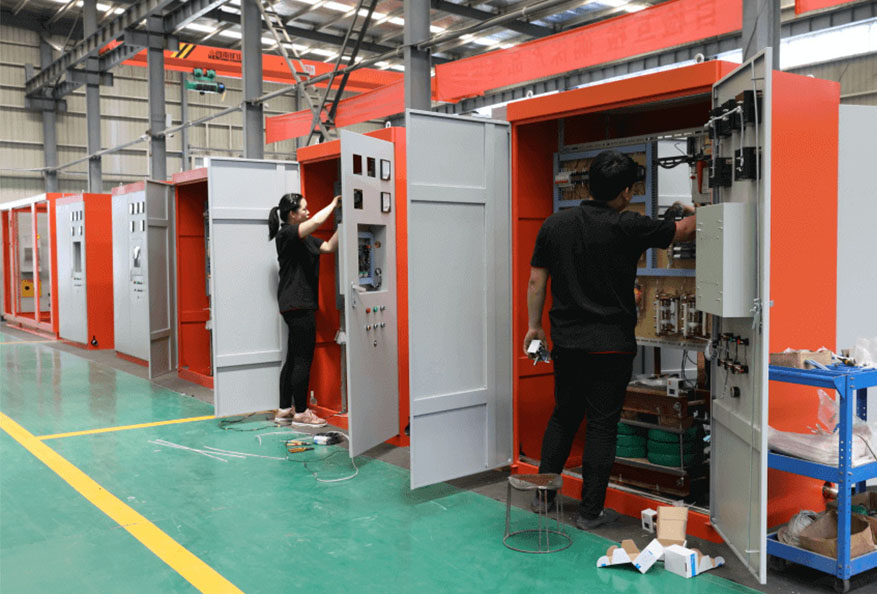
Reclamation produces fines and requires regular attention to wear components, screens, classifiers, seals, and collection points. Plan enclosed transfer points, appropriate dust collection, safe isolation, and access routes from the start. A compact layout that cannot be serviced safely is not a productive layout.
Ask for maintenance tasks to be demonstrated during design review. Consider how a screen is removed, where accumulated material is cleaned out, how lockout is applied, and whether inspection points can be reached without conflicting with normal production traffic. These details often determine whether a line retains its designed performance after the first months of operation.
For broader line planning and integration support, review our foundry equipment services before finalizing the equipment scope.
Run a representative acceptance trial
Use representative return sand and a documented operating window. Record feed rate, reclaimed output, temperature, fines handling, power use, and the quality checks that matter to your process. The objective is to establish an achievable operating baseline, not to assume identical results for every production mix.
Acceptance criteria should separate equipment capability from the foundry’s future optimization work. The trial can confirm that the delivered configuration performs within the agreed scope, while longer-term work can refine binder additions, return ratios, and operating recipes. This distinction keeps the project measurable and avoids promising an outcome that depends on untested production variables.
| Acceptance question | Practical evidence |
|---|---|
| Can the line handle peak return flow? | Timed trial with documented feed conditions. |
| Is reclaimed material suitable for the target reuse plan? | Agreed laboratory and molding-process checks. |
| Can operators maintain the line safely? | Access, isolation, and cleaning review. |
Turn process data into a clear request for quotation
A useful RFQ describes the sand and binder system, flow range, desired reuse approach, utilities, site constraints, and the checks required at acceptance. It gives suppliers the information needed to propose a coherent system rather than an isolated machine.
To discuss a sand-loop project, contact our engineering team with your process map, sample data, and production objectives.